About this item
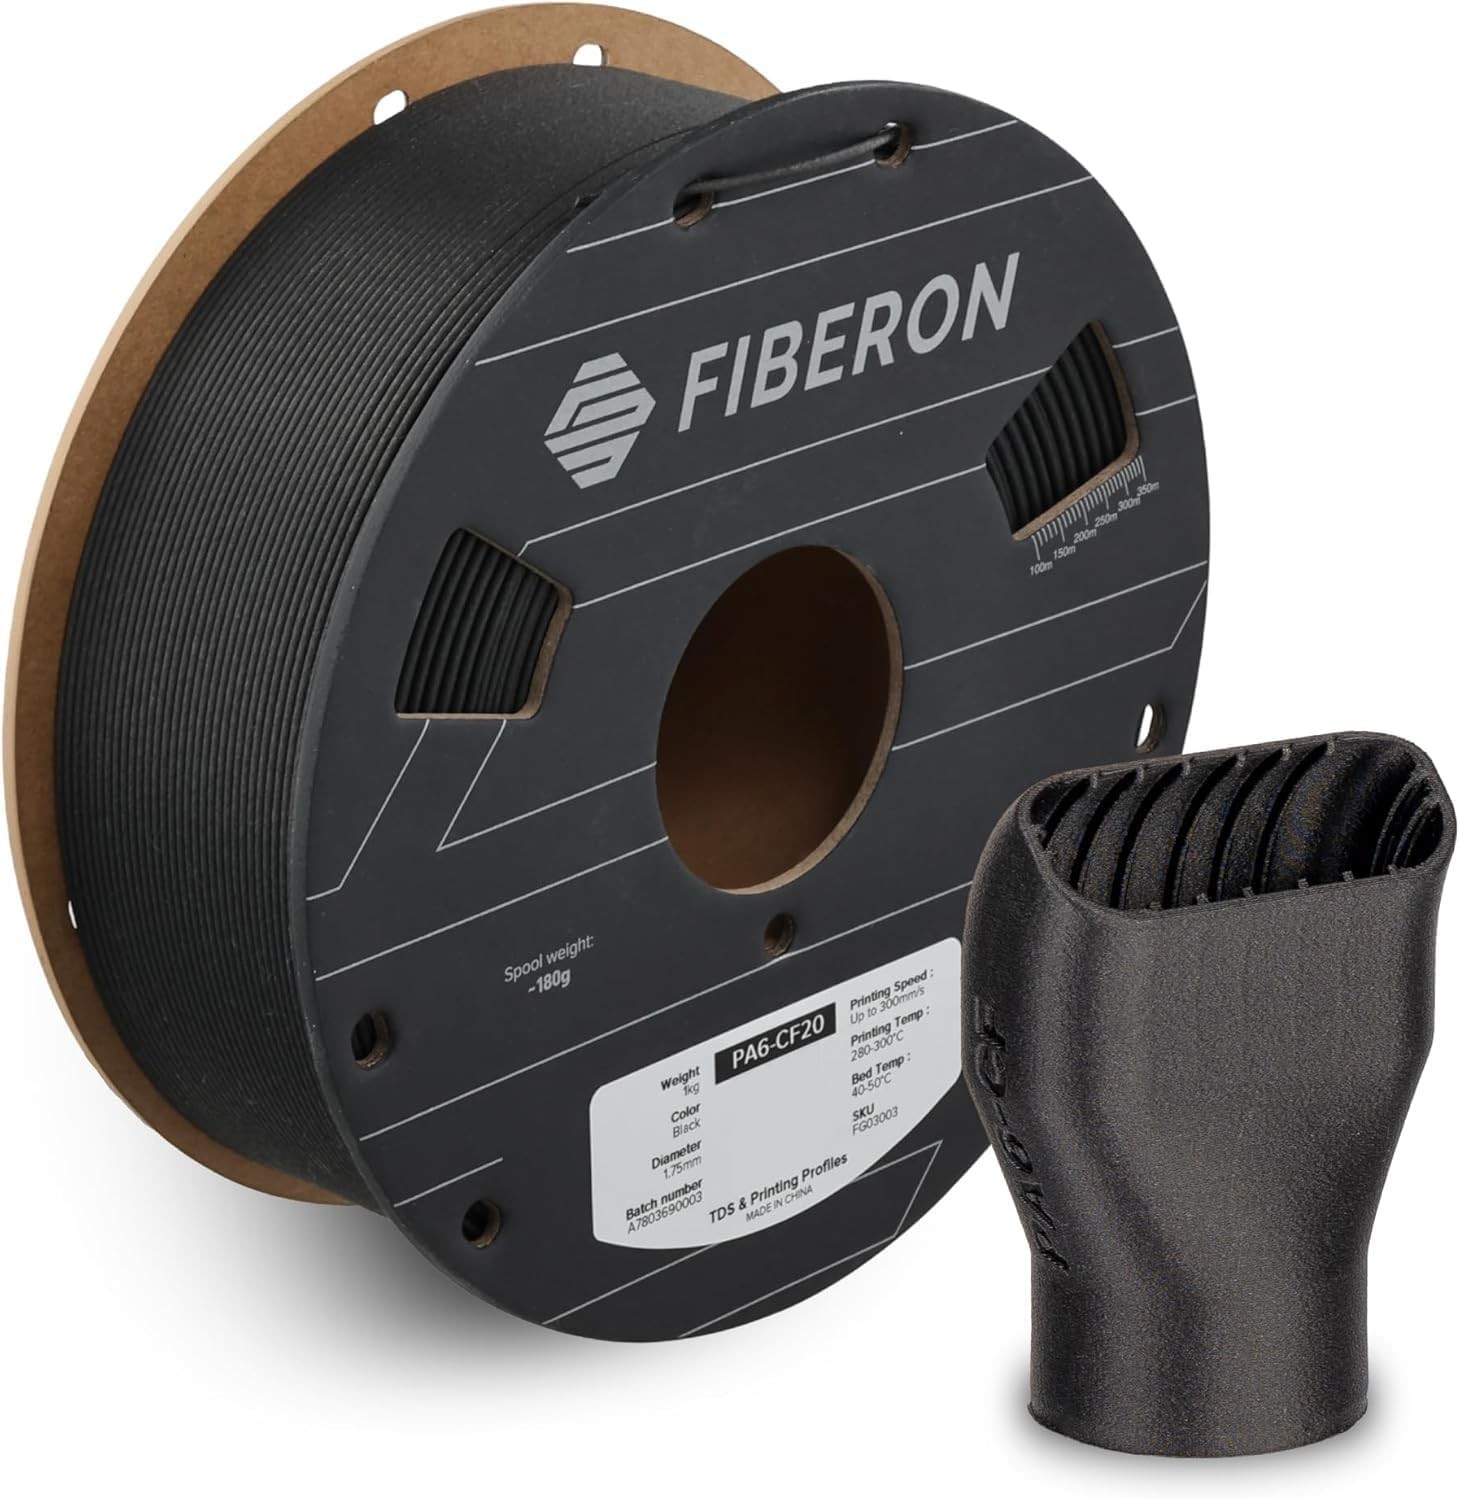
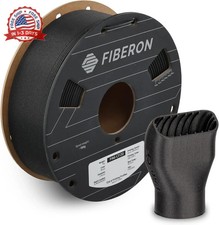
Designed for rigid functional parts, tooling, fixtures, and automotive or industrial prototypes.
Engineering Performance After Annealing: Typical TDS values include 109.3 MPa dry X-Y tensile strength and an 8.64 GPa Young’s modulus. Heat deflection temperature reaches 215°C at 0.45 MPa after annealing at 100°C for 16 hours. Final-part performance may vary with design and printing conditions.
Dry Before and During Printing: PA6 is moisture-sensitive. Dry the filament at 100°C for 10 hours before printing, then store and print below 20% relative humidity, ideally from a dry box. Proper moisture control helps reduce stringing, bubbles, rough surfaces, and inconsistent extrusion.
Advanced Printer Setup Required: Use a 280–300°C nozzle, a 40–50°C build plate, and an all-metal hotend with the cooling fan off. A heated chamber is not required; room-temperature chamber conditions are listed in the TDS. Printing speeds up to 300 mm/s are possible with a properly tuned profile.
Use a Wear-Resistant Nozzle: Carbon fiber is abrasive, so a hardened steel or ruby nozzle is required instead of a standard brass nozzle. For optimum heat resistance and dimensional stability, anneal printed parts at 100°C for 16 hours. Before long prints, confirm smooth filament routing and unrestricted spool rotation.